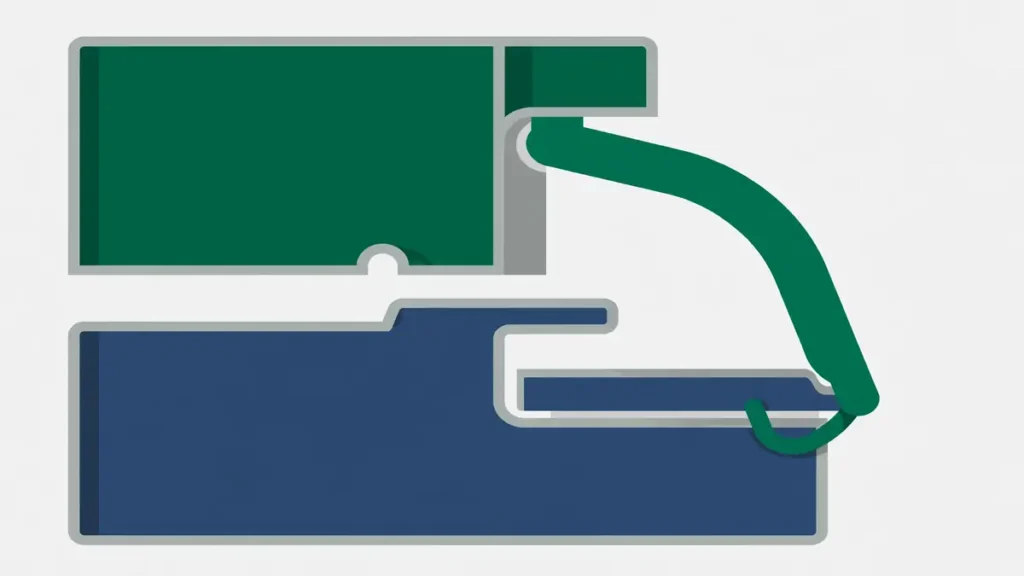
You want to close a housing without screws: no hardware, no assembly labour, no screw bosses. A snap fit does that — a hook molded into the part deflects during assembly and catches behind a ledge. When it works, the cover clicks shut and stays shut. When it does not, the hook snaps off on the first assembly, whitens and cracks after a few openings, or holds so weakly that the cover rattles open in the customer’s hands.
Size a snap fit by strain, not by how strong it looks. Choose the snap type from the job it must do, check the beam’s root strain against the resin’s permissible strain for the exact grade, and design the mold release — lifter, slide, shutoff, or collapsible core — at the same time as the hook. A snap that assembles easily but relaxes, cracks, or releases under load is not a successful design.
How to use this guide: the first table is the specification — write these six requirements down before you draw a hook. The type table chooses the snap from the job. The worked example sizes a cantilever beam against published permissible-strain values. The tooling section prices the consequence, and the last section is the trial acceptance checklist.
First, write down what the snap must do
Most snap-fit failures start before any geometry is drawn: the drawing says "add four clips" and nothing about what the clips must do. A snap fit has to satisfy several requirements at once — assembly, retention, removability, cycle life, environment — and they pull in different directions. Covestro’s Snap-Fit Joints for Plastics — A Design Guide lists mechanical load during assembly and the force required for assembly as primary design factors, and the same logic applies to every requirement below: if it is not specified, it cannot be checked.
| Requirement | What to specify | Why it matters |
|---|---|---|
| Retention | What the snap holds, against what load, and in which direction | A snap that holds a cover against gravity is a different design from one that holds a housing against a pull-out force. |
| Assembly force | The maximum force allowed to close the joint — by hand or by machine | Too high and the assembly line cannot close it; too low and it may not stay locked. |
| Removability | Separable or permanent, and how it is opened | A 90° return angle locks permanently; a shallower angle lets the joint open again. Decide before drawing the hook. |
| Assembly cycles | How many times the joint will be opened and closed in service | A one-time assembly can use far more of the resin’s strain capacity than a joint opened weekly. |
| Temperature and environment | Service temperature range, chemicals, moisture, UV | Permissible strain falls with temperature and with moisture in some resins; a snap sized at room temperature can fail in a hot car. |
| Gap and rattle | The allowable gap, rattle, or movement after assembly | A snap that holds but rattles is a quality complaint, not a pass. |
Write these six lines into the RFQ. A supplier who receives them can size the snap, choose the type, and quote the tooling. A supplier who receives only "four clips" has to guess — and the guess is usually the cheapest geometry, not the one that survives your product’s life.
Choose the snap type from the job
Covestro’s guide reduces the many possible snap joints to four basic shapes, and the choice follows the load path and the part geometry — not appearance. The table below adds the tooling consequence of each type, because the snap you choose decides what the mold must contain.
| Snap type | How it works | Best for | Tooling consequence |
|---|---|---|---|
| Cantilever | A beam projecting from the wall bends during assembly and its hook catches behind a mating ledge. Load is mainly flexural. | Housings, covers, panels, battery doors — the most common snap. | Usually mold-friendly when aligned with the draw direction; the hook is an undercut that may need a lifter, a slide, or a shutoff. |
| U-shaped | A variation of the cantilever: the arm doubles back on itself, giving a longer effective beam in a short space. | Lids and covers where there is no room for a long straight beam. | Same as a cantilever, with more steel around the folded arm. |
| Torsion | A rocker twists an integral torsion bar to open the joint; shear carries the load. | Manually releasable covers and buttons where bending space is limited. | The torsion bar and rocker need space and a clean release direction; less common, so confirm the mold layout early. |
| Annular | A continuous ring around a cylindrical part stretches radially over a bead and snaps into a groove. The whole circumference holds. | Caps, lenses, sleeves, round housings, ball-and-socket features; can give a semi-hermetic seal. | The ring is an undercut on the core side and typically needs a lifter or a collapsible core. A simple two-plate mold cannot release it. |
Two selection rules follow from the table. First, use a cantilever for most housing clips: it is the easiest to size, the easiest to mold, and the easiest to test. Second, use an annular snap only for round parts where the continuous seal or the uniform retention is the point — its tooling cost is the highest of the four, and a cantilever would have done the job on a flat panel for less.
Size the cantilever with strain, not with force
A cantilever snap fails at the root of the beam, where the bending strain is highest. The sizing check is therefore a strain check: the strain the beam sees during assembly must stay below the resin’s permissible strain for the exact grade, at the service temperature, for the required number of cycles. Covestro’s guide is built on this principle — because the snap is briefly loaded beyond the linear stress-strain range, the strain-dependent secant modulus replaces a single elastic modulus in its calculations.
For a simple rectangular, constant-thickness cantilever with small deflection, the screening estimate for the maximum root strain is:
ε = 1.5 × y × h / L²
where ε is the outer-fibre strain at the root, y is the required tip deflection, h is the beam thickness at the root, and L is the free beam length. The example below is a clearly-labelled worked calculation with stated assumptions — it ranks a design, it does not certify one.
Assumptions (stated): rectangular constant-section beam; small deflection; one mating part rigid (the other takes the full deflection); room temperature; short-term, single assembly. Final dimensioning must use the exact resin grade’s permissible strain, temperature, conditioning, and cycle requirement.
| Input | Value |
|---|---|
| Free beam length, L | 20 mm |
| Beam thickness at root, h | 1.5 mm |
| Required tip deflection, y | 1.2 mm |
| Calculation | ε = 1.5 × 1.2 × 1.5 / 20² = 2.7 / 400 |
| Result | ε = 0.00675, or 0.675% |
Now compare that result with Covestro’s published guide values for permissible short-term strain at 23 °C, for a single joining operation (from Table 2 of the guide — guide values for Covestro’s own grades, not universal allowables):
| Covestro grade family | Permissible short-term strain, single joining |
|---|---|
| Makrolon polycarbonate (PC) | 4% |
| Apec high-heat PC | 4% |
| Bayblend PC/ABS | 2.5% |
| Makroblend PC | 3.5% |
| Makrolon PC, 10% glass fibre | 2.2% |
| Makrolon PC, 20% glass fibre | 2.0% |
The worked example’s 0.675% sits well below even the lowest value in the table — so this beam, in any of these grade families, would pass the strain check for a single assembly. For a joint that is separated and rejoined frequently, Covestro advises using about 60% of these values — 1.5% for Bayblend PC/ABS, 2.4% for Makrolon PC — and the example still passes. If your numbers do not pass, the formula tells you exactly what to change: doubling the beam length cuts the strain to one-quarter; halving the thickness cuts it by half. Make the beam longer and thinner before reaching for a more flexible resin.
One warning about the numbers: they are guide values for Covestro’s grades at 23 °C. They must not be copied to an unrelated polymer or supplier grade, and they must not be treated as Cavity Mold capability. The grade you actually mold — its supplier, its filler content, its conditioning — has its own permissible strain, and that is the number the final design must use.
Three details that decide whether the snap survives assembly
The strain calculation sizes the beam. Three construction details decide whether the molded snap actually achieves that calculation in production.
Taper the beam. A constant-thickness cantilever concentrates strain at the root. Covestro’s guide recommends tapering the thickness or the width from the root to the hook — reducing the thickness linearly so it is half the root value at the hook — so the strain spreads evenly along the beam instead of peaking at one point. In the guide’s comparison, the constant-section arm uses 17% more material and exhibits 46% higher strain than the tapered design. Taper the thickness toward the tip; do not leave a uniform beam.
Give the root a radius — but not too large a radius. A sharp corner at the beam root concentrates stress and starts cracks. Covestro’s guide shows the optimum stress-concentration reduction at a radius-to-thickness ratio (R/h) of about 0.6 — but a radius that large creates a thick section at the root, which can sink or void and carry high residual stress. The guide’s compromise: reach for a generous radius, accept that the optimum is a trade-off against sink, and never use a radius below 0.015 in (0.38 mm) in any instance.
Set the lead and return angles separately. The hook has two faces: the lead-in angle the mating part slides over during assembly, and the return angle that holds it after engagement. A shallow lead-in angle (around 20–30° from the axis) eases assembly; a steep return angle (45–90°) resists pull-off. A 90° return face locks the joint permanently — the only way out is to break it. Decide removability first (see the requirements table above), then set the return angle to match.
Keep weld lines, ejector marks, and texture transitions out of the high-strain root area. A weld line at the root is a ready-made crack starter, and an ejector pin mark on the beam is a stress concentrator in exactly the wrong place. Raise both at the design review.
What a snap fit costs in tooling
A snap fit is cheap in parts and can be expensive in steel. The hook is an undercut — a feature the mold cannot release by simply opening — and the tool must contain a mechanism to form and release it. Ask about the mechanism in the quotation, because it is where the snap’s cost lives.
| Release method | When it is used | What it means for the buyer |
|---|---|---|
| Shutoff (pass-through core) | The hook can be formed by two mold faces meeting, with no side movement | The cheapest release — no mechanism. Ask whether your hook geometry allows it; a small redesign of the hook can sometimes make a shutoff possible. |
| Lifter | The hook is on an angled lifter that moves with ejection | The common solution for cantilever hooks. Adds steel, machining, and maintenance to the mold. |
| Slide (side action) | The undercut is on a side face and needs a moving core | Needed when the hook cannot be reached by a lifter. More steel and more maintenance than a lifter. |
| Collapsible core | An annular snap needs the core to collapse inward to release the ring | The standard solution for annular snaps, and the most expensive of the four. |
| Bump-off | A small undercut in a flexible resin is stripped off the core by the part flexing during ejection | Possible only for small undercuts in flexible materials. It stresses the part on every cycle — confirm the undercut size and the resin allow it. |
Two cost questions to ask in the RFQ. First, "which release method does each snap need, and what does it add to the tool?" — so the tooling cost is visible before the order, not discovered in the quote. Second, "what happens to the snap if the undercut depth changes?" — because a snap that needs a collapsible core at 0.6 mm of undercut may need only a lifter at 0.3 mm, and the design trade is worth making before steel is cut. Our draft-angle guide makes the same point from the draft side: do not hide an undercut inside a nominally drafted wall, because the undercut will need a slide, a lifter, or a design change — and the design change is cheapest before tooling.
Prove it at the first trial
A snap fit cannot be approved by looking at it or by closing it once. It must be assembled, pulled, opened, and assembled again — and the numbers recorded. Add these checks to the trial acceptance; our T1 approval guide explains the approval sequence, and the items below are the snap-specific checks that go inside it.
| Check | What to do | Pass looks like |
|---|---|---|
| Assembly force | Close the joint with the intended method (hand or fixture) and record the force. | Within the specified maximum, and consistent across parts and cavities. |
| Retention force | Pull or push the joint in the direction it must resist, and record the force at which it releases or fails. | Meets the specified minimum, with margin — not barely, and not by breaking the hook. |
| Cycle test | Open and close the joint for the cycle count you stated in the RFQ, or an agreed sample count with the count recorded. | No crack, no whitening at the root, no loss of retention force, no permanent set that leaves a gap. |
| Whitening and crack check | Inspect the beam root and the hook in good light after the cycle test. | No white stress marks and no cracks. Whitening is a strain warning, not a cosmetic issue. |
| Undercut measurement | Measure the hook undercut and the mating ledge on the trial parts and compare with the drawing. | Within tolerance, and consistent across cavities — an undercut that varies by cavity gives snaps that vary by cavity. |
| Gap and rattle | Assemble the parts and check the gap, the fit, and any movement. | No gap beyond the specified allowance, no rattle, no rocking. |
| Material certificate | Confirm the resin grade and lot on the trial parts match the drawing. | The exact grade specified — a grade change after approval needs a new snap review. |
If the snap fails the cycle test, do not accept the parts and "fix it later". The usual corrections, in order: a longer beam, a thinner beam, a larger root radius, a tapered beam, a different lead angle — one change at a time, so the next trial shows which change worked. And remember what a sample cannot prove: a trial proves the snap works on trial parts. It does not prove the snap will work after a grade change, a tool repair, or a year’s production — so the acceptance criteria, the grade, and the undercut measurement belong in the production records, not only in the trial report.
Frequently asked questions
Can a snap fit be opened again after assembly?
Only if it was designed to be. A shallow return angle lets the hook slide back out; a 90° return face locks it permanently. Decide removability before the hook is drawn — changing it later means changing the tool.
The snap whitens at the root but does not break. Is that a pass?
No. Whitening is local yielding: the strain at the root has exceeded what the resin tolerates, and the snap will crack after more cycles. Treat whitening as a failure, lengthen or thin the beam, enlarge the root radius, and re-test.
Snap fits or screws — which is cheaper?
Per part, a snap fit is usually cheaper: no hardware, no screw bosses, no assembly labour. Per tool, it can be more expensive, because the undercut needs a lifter, slide, or collapsible core. Compare the total program cost — tooling plus parts plus assembly — at your actual volume, not the part price alone. Our order-quantity guide explains how volume changes the part-price side of that comparison.
Send the drawing and your snap requirements
A snap fit is a small feature that decides whether the product feels well made or falls apart in the customer’s hands. Send us the CAD file and the 2D drawing with the snap locations marked, the retention and assembly-force requirements, whether the joint must be removable, how many times it will be opened and closed, the material grade if you have fixed one, the annual volume and order quantity, and your delivery region and timing — and we will review the snap type, the beam size, and the mold release with you before tooling starts, so the first trial tests a snap that has a chance of passing.
Contact Cavity Mold with your drawing and snap requirements.