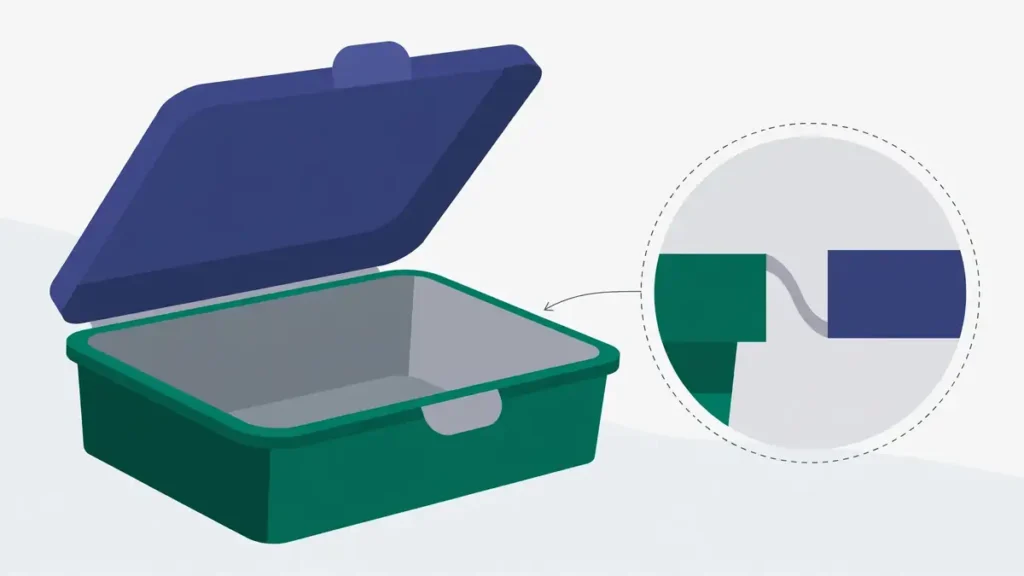
Your part needs a lid that opens and closes — a storage box, a cap, a case, an appliance door. You could add a metal pin hinge and an assembly step, or you could mold the hinge as part of the part itself: a thin web of plastic that bends thousands of times. When it works, it is the cheapest hinge you will ever buy. When it fails, it usually fails on the first day, snapping the first time someone opens the lid.
A living hinge survives when three decisions are all right: the material must be a flexible, fatigue-resistant resin — polypropylene first; the hinge must be thin, typically 0.2–0.5 mm, with generous radii; and the mold must be gated so the melt flows across the hinge, orienting the polymer chains in the direction of bending. Get any one of the three wrong and the hinge will crack early, however good the other two are.
How to use this guide: the first table decides whether a living hinge is the right choice at all. The geometry table gives you the four numbers your drawing must carry. The worked example shows why halving the hinge thickness roughly halves the bending strain. The last two sections tell you what to write in the RFQ and how to test the hinge at the first trial.
Is a living hinge the right choice for your part?
A living hinge is a thin, flexible strip made from the same material as the connected parts, with no hardware and no assembly. That simplicity is the whole point — and it is also the limit. It carries light loads, it bends in one plane, and it depends entirely on the resin and the geometry. Before you design one, check that the job fits.
| Requirement | Living hinge | Mechanical hinge (pin, knuckle, hardware) |
|---|---|---|
| Cost and part count | One molded part, no hardware, no assembly step | Separate parts, hardware, and an assembly operation |
| Cycle life | Very high when designed correctly — a well-designed injection-molded polypropylene hinge can reach millions of flexes (Fictiv) | High, but friction and wear at the pin grow over time |
| Load | Light loads only — lids, caps, covers, cases | Structural loads, heavy doors, controlled resistance |
| Motion | One bending plane, one axis | Controlled rotation, detents, friction stays possible |
| Design effort | High — material, geometry, and gate direction must all be right | Low — the hinge is a bought or standard component |
| When it wins | High-volume consumer parts where cost and simplicity matter | When the hinge must carry weight, hold a position, or survive abuse |
If the lid must stay open at a fixed angle, hold weight, or survive being forced past its stop, a living hinge is the wrong choice — say so in the RFQ and ask for a mechanical hinge instead. If the job is a lightweight lid that opens and closes in normal use, the living hinge is usually the better answer, and the rest of this guide is how to specify it.
Start with the material: polypropylene first, polyethylene second
No geometry can save a living hinge made from the wrong resin. The hinge works because the thin section is ductile enough to bend repeatedly without cracking — and only a few resins are.
| Material | Hinge behaviour | When to use it |
|---|---|---|
| Polypropylene (PP), homopolymer | The standard. High flexural fatigue resistance; a well-designed injection-molded PP hinge can reach millions of flexes. | First choice for any hinge that must open and close many times. |
| Polyethylene (PE) | Similar in character to PP, slightly less robust in fatigue. | Second choice, where the part is already PE for other reasons. |
| ABS, polycarbonate, rigid blends | Rigid plastics with low fatigue resistance at thin sections. A hinge in ABS may survive a few hundred cycles and then crack. | Do not specify a high-cycle living hinge in a rigid resin. If the part must be ABS, use a mechanical hinge. |
| Glass-filled grades | Fillers raise stiffness and cut fatigue life sharply at the hinge. | Avoid for the hinge section; if the part needs a filled grade elsewhere, discuss a two-material solution before tooling. |
Two details about the grade matter as much as the family. First, homopolymer PP is the usual choice for hinges, and the grade should have a high enough melt flow rate to fill the thin hinge section reliably — confirm both points with the resin supplier’s data for the exact grade. Second, name the exact grade on the drawing and in the RFQ: "PP" is a family, not a specification. Our material selection guide makes the same point for resin choice in general — the grade, not the family name, controls the result — and it recommends PP first for living hinges for exactly the fatigue reason above. Do not change the grade after the mold is built without a new hinge review: the mold is designed around the shrink and flow behaviour of one resin.
The four numbers that decide whether the hinge survives
A living hinge is defined by four geometric parameters. Each one has a starting range from published design guidance — Fictiv’s guide gives the thickness range and the T = H/5 to H/8 rule below; the land and radius ranges are the starting values used across published hinge guidance. Each parameter fails in a different way when it is wrong, and the final values must be confirmed against your grade’s data sheet and the trial.
| Parameter | Starting range | What happens if it is wrong | Where it goes on the drawing |
|---|---|---|---|
| Hinge thickness (t) | 0.2–0.5 mm | Too thick: the surface stretches past its limit on each bend and the hinge cracks early. Too thin (below ~0.2 mm): the hinge may tear during molding or ejection. | Nominal thickness with a tolerance — and the tolerance matters: a hinge that molds 0.1 mm thicker than drawn is a different hinge. |
| Land length (L) | 0.5–1.5 mm of thin section | Too short: the bend concentrates at one line and the strain peaks there. Too long: the hinge feels loose and the lid does not close crisply. | The length of the thin section, measured along the bending direction. |
| Bend radius (R) | Generous radii on both sides of the web, typically 0.25–0.75 mm or more | Sharp corners where the web meets the rigid wall concentrate stress and start cracks after a few hundred cycles. | Minimum radius callouts at both transitions from web to wall. |
| Hinge length (along the axis) | As short as the part allows; hinges longer than about 150 mm (6 in) should be split into two or more sections | One very long hinge fills unevenly and bends unevenly — one end takes the strain and fails first. | The hinge span, and the split points if the hinge is divided. |
Two rules of thumb from Fictiv’s living hinge design guide are worth writing into your design notes. First, hinge thickness can be estimated from the adjoining wall: T = H/5 to H/8, where T is the hinge thickness and H is the thickness of the adjoining material — so a 2.4 mm wall suggests a hinge of 0.3–0.48 mm. Second, for a 180° bend, the land length and the bend radius are linked by L = πR: the hinge should form a semicircle when closed, so the strain spreads evenly instead of peaking at one point.
Fictiv also recommends two construction details that are easy to miss in CAD. Add "shoulders" — a flat recess on either side of the hinge — so the hinge bends in the centre and the part has room to close. And start thin: it is easier to thicken a hinge by removing tool steel than to thin one by adding it, so a steel-safe start protects your options at trial.
Worked example: what halving the thickness does to the strain
The reason a thin hinge lasts longer is not that thin plastic is stronger — it is that a thinner section bends with less surface strain. For a bent section, the outer-fibre strain can be estimated with the beam-theory relation ε ≈ t / (2R), where t is the hinge thickness and R is the bend radius. The example below is a clearly-labelled screening comparison, not a pass/fail test: it compares two thicknesses at the same radius so you can see the size of the effect.
Assumptions (stated): a uniform bend radius R = 1.0 mm; the hinge bends as a simple curved beam; room temperature; one bend. Real hinge strain also depends on the land geometry, the transition radii, the resin grade, the temperature, and the number of cycles — so this example ranks designs, it does not certify one.
| Hinge | Calculation | Surface strain |
|---|---|---|
| t = 0.25 mm | ε ≈ 0.25 / (2 × 1.0) | ≈ 0.125, or 12.5% |
| t = 0.50 mm | ε ≈ 0.50 / (2 × 1.0) | ≈ 0.25, or 25% |
Doubling the thickness doubles the surface strain on every bend — which is why a hinge that looks more robust at 0.5 mm can fail sooner than a 0.25 mm hinge in the same part. The trade-off is stiffness: the thinner hinge bends more easily, so the lid closes with less resistance and may feel loose. That is a product decision, not a molding decision — decide how firmly the lid must stay closed, then pick the thinnest hinge that still holds it.
One more reason the numbers above are only a screening estimate: a living hinge survives because the polymer chains in the thin section are oriented by flow during molding, and oriented polypropylene stretches far further than bulk polypropylene before it fails. That orientation is set by the gate — which is the subject of the next section.
Gate placement: the decision that makes or breaks the hinge
If there is one decision that decides hinge life, it is where the melt enters the mold. When molten plastic flows through the thin hinge section, the polymer chains align in the direction of flow. For the hinge to bend without breaking, those chains must run perpendicular to the hinge axis — in the direction the hinge opens and closes. Flow along the hinge axis, parallel to the centreline, leaves no orientation in the bending direction, and the hinge can fail after a handful of cycles.
What to agree with the mold maker before steel is cut:
- Gate so the melt flows across the hinge, not along it. The gate position is a design requirement, not a mold-maker preference — write "melt flow across the hinge" on the drawing or in the RFQ, and ask for the gate layout to be shown at the design review.
- Prefer a fan gate for a long hinge. A fan gate spreads the flow evenly across the hinge length, so the whole hinge fills and orients at the same time.
- Keep weld lines away from the hinge. A weld line — where two flow fronts meet — in the thin section is a ready-made crack starter. If the part geometry forces a weld line near the hinge, raise it at the design review and ask for the gate layout to be changed.
- Decide whether the part molds open or closed. A cap whose two halves close together may need to be molded open, or at an angle, for the tool to release as one piece. Agree the molded position before tooling — it affects the hinge geometry and the ejection.
- Flex the hinge immediately after ejection, while the part is still warm. Flexing a few times right after molding cold-draws the plastic and greatly increases the hinge’s service life. Ask that this step be part of the trial procedure, not left to chance.
If the gate layout cannot put flow across the hinge — because of the part shape, the cavity layout, or a multi-cavity tool — say so early. A hinge with the wrong flow direction is a design change, not a process tweak, and it is far cheaper to fix before the mold is built than after the first trial parts snap.
What to put on the drawing and in the RFQ
A hinge that exists only as a thin section in the CAD model, with no numbers attached, will be molded to whatever the toolmaker guesses. Write these into the drawing and the RFQ so the hinge is a specification, not an assumption:
- Hinge thickness, with tolerance — nominal 0.2–0.5 mm for PP, and a tolerance tight enough that the molded hinge is the hinge you designed. Ask how the thickness will be measured and verified.
- Land length and transition radii — the length of the thin section and the minimum radius where it meets each rigid wall.
- Material grade, named exactly — homopolymer PP, grade and supplier, melt-flow rate, and colour. State whether a grade change is allowed without a new hinge review (it should not be).
- Gate direction requirement — "melt flow across the hinge" and the gate type, agreed at the design review.
- Open angle and cycle requirement — how far the hinge must open, and how many open/close cycles the product needs in its expected life. State your own number; do not ask the supplier to invent one.
- Hinge length and split points — the span, and where the hinge is divided if it is long.
- What the trial must prove — the flex test in the next section, written into the trial acceptance criteria.
Our bottle-cap guide shows the same discipline applied to a closure: thread form, seal land, torque target, and a release strategy for the thread, all defined before mold engineering. A hinge deserves the same treatment — it is the feature most likely to fail first.
How to test the hinge at the first trial
A hinge cannot be approved by looking at it. It must be flexed, measured, and flexed again. Add these checks to the trial acceptance — our T1 approval guide explains the approval sequence; the items below are the hinge-specific checks that go inside it.
| Check | What to do | Pass looks like |
|---|---|---|
| Flex warm, then cold | Flex each hinge a few times while the part is still warm from the mold, then again after it has cooled to room temperature. | No cracking, no whitening, no stiffness change between warm and cold flexing. |
| Cycle test | Open and close the hinge to the full design angle for the cycle count you stated in the RFQ — or, if the full count is impractical at trial, an agreed sample count with the count recorded. | No crack, no whitening at the web or the radii, no loss of closing force, no change in hinge thickness. |
| Whitening check | Look closely at the hinge web and both transition radii after the cycle test, in good light. | No white stress marks. Whitening is the hinge telling you the strain is too high — it is a failure warning, not a cosmetic issue. |
| Thickness measurement | Measure the molded hinge thickness at several points along its length and compare with the drawing. | Within the drawing tolerance, and consistent along the length. A hinge that is 0.1 mm thicker at one end will fail at the other end first. |
| Gate-direction confirmation | Confirm from the trial parts and the mold record that the gate layout gives flow across the hinge. | No weld line in the hinge section; the flow pattern, if visible, runs across the hinge. |
| Lid function | Close the lid fully and check the seal, the latch, and the closing feel. | The lid closes crisply, stays closed, and opens without forcing. |
If the hinge fails the cycle test, do not accept the parts and "fix it later" — the fix is a design or gate change, and it belongs before production, not after. The most common corrections are a thinner hinge, larger transition radii, a different gate position, or a grade change — in that order, and one at a time, so the trial can show which change worked.
Why hinges fail early
Most early hinge failures trace back to one of five causes. The table is a diagnostic shortcut: match the symptom, check the cause, and ask for the correction.
| Symptom | Likely cause | Correction to ask for |
|---|---|---|
| Hinge snaps on the first few opens | Hinge too thick; sharp corners at the web; gate along the hinge; wrong material | Thinner hinge, larger radii, gate across the hinge, homopolymer PP |
| Hinge whitens, then cracks after weeks of use | Strain too high for the cycle count; radii too small | Thinner hinge or larger bend radius; re-check the cycle requirement |
| Hinge tears during molding or ejection | Hinge too thin (below ~0.2 mm); poor ejection | Thicken slightly within the 0.2–0.5 mm range; check the ejection and the molded position |
| One end of a long hinge fails first | Uneven fill along the hinge; hinge too long for one section | Split the hinge; check the gate layout and the fan gate |
| Hinge works at trial, fails in the field | Grade changed after approval; hinge thickness drifted as the tool wore | Freeze the grade in writing; measure hinge thickness across production lots |
Frequently asked questions
Can I use a living hinge in ABS?
Not for a hinge that must open and close many times. ABS and other rigid resins have low fatigue resistance at thin sections — the hinge may survive a few hundred cycles and then crack. If the part must be ABS, use a mechanical hinge, or discuss a two-material design before tooling.
Can a living hinge be repaired if it cracks?
No. A cracked hinge cannot be repaired or reinforced in a way that restores its fatigue life. The correction is a new hinge design — thinner, better radii, better gate direction — and a new trial.
How many flex cycles should I ask for?
State the number your product needs: how many times the lid will open and close in its expected life, with a margin. A storage box opened twice a day for five years needs roughly 3,600 cycles; a cap opened daily needs roughly 2,000. Give the supplier your number and ask for the trial to prove it — do not ask them to guess it.
Send the drawing and your hinge requirement
A living hinge is a small feature with a large failure cost — it is the part of the product the customer touches every time they use it. Send us the CAD file and the 2D drawing with the hinge thickness, land length, and radii marked, the open angle and cycle count your product needs, the material grade if you have fixed one, the annual volume and order quantity, and your delivery region and timing — and we will review the hinge geometry and the gate direction with you before tooling starts, so the first trial tests a hinge that has a chance of passing.
Contact Cavity Mold with your drawing and hinge requirement.