
Key takeaway: Turning a plastic product color concept into a molded part requires a color standard, compatible resin, masterbatch trials, process control, measurement, and approved samples.
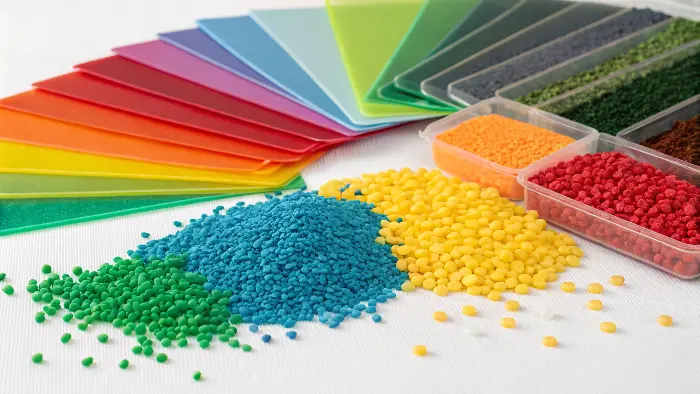
Convert the idea into a measurable target
A screen image or verbal color name is not a production standard. Define the target under controlled lighting, material, texture, gloss, and viewing conditions. Note the visible zones, acceptable variation, and whether the customer cares about color alone or also opacity, sparkle, translucency, or tactile finish.
Connect color development to tooling and process
Color appearance depends on resin grade, wall thickness, flow, cooling, texture, gloss, gate location, and processing history. Develop the color on a representative part or coupon and review the actual cosmetic zones. Mold finish should be specified alongside the color target because surface reflection changes perceived color.
Keep an approval loop: trial formulation, molded samples, instrument and visual review, correction, final standard, then production verification. This prevents a late-stage color decision from being separated from manufacturability.
Make the result repeatable
Document the approved masterbatch, resin, dosage, drying, machine conditions, inspection method, and lot controls. Plan for supplier continuity and define what happens when resin, pigment, regrind, mold texture, or process settings change.
Frequently Asked Questions
Can a brand color be specified only with a digital RGB value?
No. Digital color can guide development, but a production approval needs a physical or instrumented standard under defined material, surface, lighting, and measurement conditions.
Why does the same color look different on two molded parts?
Resin, wall thickness, texture, gloss, flow, cooling, gate location, pigment dispersion, and viewing conditions can change the appearance.
When should color be approved?
Approve it on a representative molded sample before production, with the resin, mold surface, process window, measurement method, and visual zones documented.
Related Cavity Mold Services
Engineering and DFM; Mold making; Plastic injection molding; Contact Cavity Mold.
Have a drawing, resin, finish, volume, or quality requirement to review? Contact Cavity Mold for a project discussion.
Reference material
Translate visual intent into production controls
A screen, rendering, or paint chip can start a color conversation, but a molded part needs a reference, material route, surface definition, viewing condition, and acceptance method that production can repeat.
Color-definition handoff
- Record the visual reference, intended use, viewing light, background, and acceptable variation.
- Define resin, grade, additives, colorant, texture, gloss, and expected wall range.
- Create an approved molded reference part or measured standard when possible.
- Set the reaction to drift: containment, measurement repeat, process review, or colorant correction.
Questions for the design team
What must match? Decide whether the requirement is hue, lightness, chroma, gloss, effect, or brand appearance.
Where is the color judged? State the surface, part thickness, lighting, angle, and assembly context.
What can change? Define approved resin, colorant, texture, and process substitutions before launch.
Use engineering to make the color brief measurable before the production RFQ.