Key takeaway: Injection mold polishing defects such as orange peel, pitting, drag lines, rounded edges, and over-polishing need steel, abrasive, geometry, process, and inspection evidence.
Classify the defect before repolishing
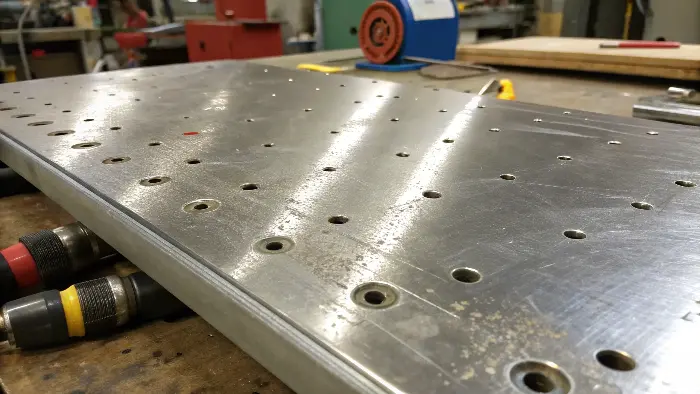
Orange peel, pits, drag lines, haze, scratches, rounded edges, and an over-polished appearance can have different causes. Record the location, steel, previous abrasive stage, tool direction, geometry, lighting, and whether the issue is visible in the molded part. Repolishing without classification can enlarge a pit or remove a critical edge.
Use a named finish standard and a consistent inspection method. Surface classifications are helpful references, but a part-level cosmetic requirement must describe where and how the defect is judged.
- Mark the defect on the mold and part.
- Separate steel, process, material, and inspection symptoms.
- Retain an approved reference for comparison.
Find the process cause
Pitting may point to steel or polishing contamination, corrosion, inclusions, or local damage; orange peel can reflect an uneven surface or abrasive sequence; rounded edges often indicate excessive pressure or uncontrolled access. Molded-part defects can also come from flow, cooling, resin, or handling rather than the polish itself.
Inspect the surface progressively and check the polishing tools, abrasive cleanliness, pressure, direction, and stage changeover. Correct the source before moving to a finer finish.
- Check steel and EDM or machining preparation.
- Control abrasive cleanliness and sequence.
- Protect edges, vents, shutoffs, and engraved details.
Confirm the correction in production conditions
After correction, mold representative material and color and inspect the critical zone under the agreed lighting. Check dimensions and release as well as appearance. Record the correction, finish reference, sample result, and any approved limit so the same defect is not recreated during maintenance.
- Compare mold and molded-part evidence.
- Check the full cosmetic zone, not only the repaired spot.
- Update the maintenance and change record.
Frequently Asked Questions
Why can over-polishing be a defect?
Removing too much steel can round edges, widen gaps, change shutoffs, alter geometry, or create a surface that no longer matches the intended appearance.
Should every pit be polished deeper?
No. First identify whether the cause is steel, contamination, corrosion, geometry, or inspection; deeper polishing may make the condition worse.
How is a finish correction released?
Verify the mold and molded part under the approved inspection method, then record the correction, sample, dimensions, and any approved limitation.
Need a part-specific review? Share the 3D model, resin or grade, annual volume, finish requirement, tolerance concerns, and target launch date through our contact page. We can then align DFM, mold design, process, inspection, and delivery assumptions.
Sources and further reading
- Autodesk: Mold surface classifications
- Protolabs: Surface finishes
- Plastic Technology Alliance: Injection mold surface finish
Related Cavity Mold Services
For a connected review of design, tooling, molding, and launch requirements, see our engineering service, mold-making service, injection molding service, or contact our team.
Diagnose the surface before removing more steel
Orange peel, pits, drag marks, rounded edges, and over-polished boundaries can look similar under uncontrolled light. Record the defect pattern, starting surface, abrasive sequence, geometry, and cleaning history before correcting it.
| Decision | Evidence to review | Boundary |
|---|---|---|
| Orange peel or haze | Compare texture scale, direction, abrasive step, pressure, and molded appearance. | Do not assume more pressure will produce a better finish. |
| Pitting or pull-outs | Check steel condition, EDM recast, inclusions, porosity, and cleaning. | The defect may require steel repair rather than more polishing. |
| Over-polishing | Inspect edges, radii, shutoffs, texture boundaries, and dimensions. | A visually smooth surface can be functionally damaged. |
| Verification | Use consistent lighting, viewing angle, sample, and molded-part comparison. | Approval requires an agreed standard, not a subjective last look. |
Polishing-defect diagnosis
- Photograph or map the defect with scale and direction.
- Review the last accepted polishing stage.
- Choose the least destructive corrective action.
- Reinspect the tool and molded feature before release.
Use mold-making for the tool correction and engineering for the part-level acceptance decision.