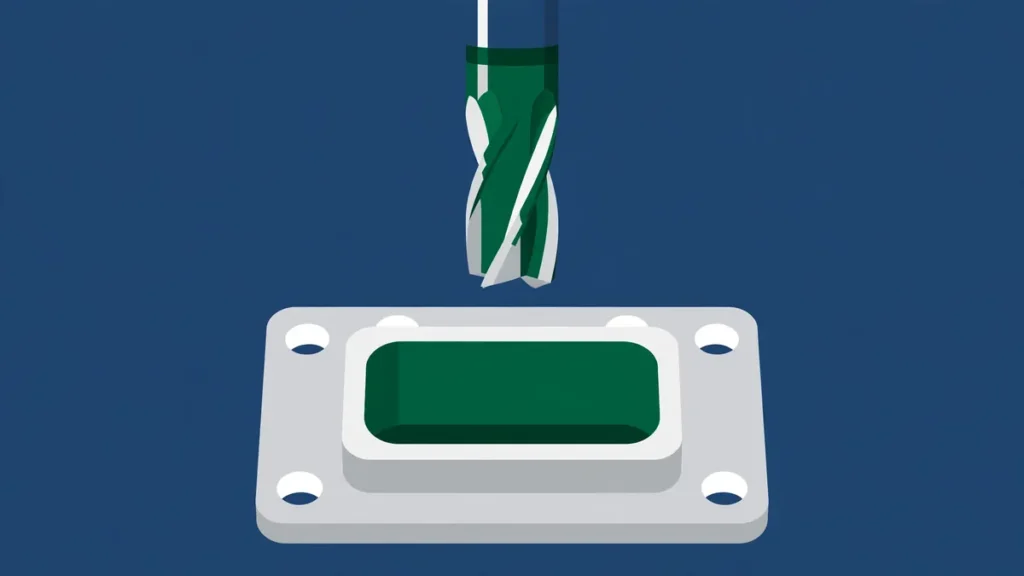
A machined part can come back quoted far higher than the buyer expected — and the drawing usually explains why: a pocket deeper than the tool can reach, or a corner sharper than any cutter.
Before you send the drawing for quote, enlarge the internal corner radii, keep pockets shallow, keep walls thick enough to stay rigid, use standard hole and thread sizes, and reduce the number of setups — after tolerances, in that order of priority. Most of the price is machine time, tool wear and handling, and each of these changes removes some of it.
How to use this guide: the design-rule table is the whole guide in one place — check your drawing against it first. The sections after it explain why each rule matters, the worked example shows one pocket redesigned, and the checklist at the end is what to run through before the drawing leaves your desk.
The design-rule table: what each rule costs if you ignore it
Every number here is a published design rule from Protolabs (US) or Protolabs Network / Hubs, written for their own services — rules of thumb, not Cavity Mold capability claims. Confirm them with the shop that will make your part.
| Feature | Common guideline | What it costs if ignored | What to change |
|---|---|---|---|
| Internal corner radius | Larger than one third of the pocket depth (Hubs); as large as possible (Protolabs) | A small cutter, slow feeds, long cutting time, and a tool that may not reach the depth at all | Enlarge the radius; use one radius for all internal corners so the shop does not change tools |
| Pocket depth | No deeper than 4 times the pocket width (Hubs) | A long, thin cutter that deflects and vibrates, more passes, slower feeds, risk of scrapping the part | Make the pocket shallower, wider, or split the depth across a step; check whether the depth is really needed |
| Wall thickness | At least 0.8 mm for metals, 1.5 mm for plastics (Hubs); Protolabs’ minimum is 0.5 mm | Vibration and deflection during cutting, looser tolerances, parts that move after unclamping | Thicken the wall, add a rib, or accept a looser tolerance on that feature |
| Tall features | Height less than 4 times the width (Hubs) | Vibration, poor surface finish, dimensions that drift | Shorten the feature, widen its base, or rotate the part so the feature is machined lying down |
| Hole diameter and depth | Standard drill sizes; depth no more than 4 times the diameter, 6 times at most (Hubs) | An end mill instead of a drill, slower cutting, a tool that cannot reach, or a hole drilled from both sides | Use a standard drill size; shorten the hole, enlarge the diameter, or make it a through hole |
| Thread size and length | M6 or larger, length no more than 3 times the diameter (Hubs) | A small tap or thread mill, breakage risk, and a thread that cannot be cut to the depth asked for | Use a larger thread, shorten the engagement, or use an insert — see our guide on how to specify threads on CNC machined parts |
| Small features | No smaller than 2.5 mm where possible; 0.5 mm is the feasible limit (Hubs) | Micro-machining, special tooling, slow feeds, and a feature that may not survive handling | Enlarge the feature, or ask whether it is needed at all |
| Setups | One or two setups on a 3-axis mill (Hubs) | Manual repositioning, re-alignment error, extra fixturing, and a second round of inspection | Put features on as few faces as possible; split the part into two pieces that assemble |
| Stock size | Close to the finished part size | Every millimetre of extra stock is material bought and then cut away | Choose the smallest standard stock that covers the part plus clamping allowance |
| Cosmetic faces | Mark them; leave the rest as-machined | Paying for a fine finish on faces nobody sees | Name the cosmetic faces on the drawing and leave the rest at the standard finish |
Why these rules change the price
A CNC quote is mostly a price for time — cutting, setup, tool changes, and inspection — with material usually the smaller part of the bill. A design change saves money when it shortens one of those times.
Machine time is the biggest lever. A cutter removes material at a rate set by its size, stiffness, and depth of cut: a large, short, rigid cutter removes far more per pass than a small, long, flexible one, and moves faster without vibrating. That is why the same pocket costs far more with a 1 mm corner radius than with a 10 mm one — the radius decides the cutter, and the cutter decides the speed. Protolabs makes the same point: its milling cutters go down to 1 mm, but a pocket cut with a tool that small is limited to about 9.52 mm deep.
Setups are another lever. Every time the part is taken off the machine, turned over, re-clamped and re-aligned, somebody is doing manual work and the machine is not cutting. Hubs’ cost guidance is plain: design parts for one or two setups on a 3-axis mill, or split the part into pieces machined in one setup each. The alternative is multi-axis machining, but Hubs’ published relative costs put indexed 5-axis work about 60% above 3-axis milling and continuous 5-axis about 100% above it.
Inspection is the last lever: every tight tolerance is a measurement somebody has to make. Our guide to CNC tolerances explains the ISO 2768 default — tighter limits belong only where fit, function, sealing or alignment genuinely demands them.
Corner radii: the cheapest change you can make
A milled pocket cannot have a sharp internal corner: the cutter is round, so the corner it leaves is round too, with a radius a little larger than half the cutter’s diameter. A drawing that calls for a sharp corner asks for something the mill cannot do.
Hubs’ rule: make the internal radius larger than one third of the pocket depth, and larger is better. Protolabs says the same in plainer terms — relieve the internal corners, or allow for as large a radius as possible. A 10 mm deep pocket with a 1 mm corner radius needs a cutter no larger than 2 mm in diameter, and a 2 mm cutter that long is flexible: it deflects, vibrates, and takes shallow, slow passes. The same pocket with a 10 mm radius takes a 20 mm cutter, which is rigid and removes far more material per pass.
Two habits make the change pay off fully. First, use the same radius on every internal corner: one radius means one cutter and no tool changes. Second, do not put a radius where the design needs a square corner — if a mating part must sit flat against the pocket wall, a radius leaves a gap. The fix is an undercut, a small relief cut so the mating part can seat.
The pocket floor deserves the same attention: Hubs recommends its edges be sharp or given a 0.1 mm or 1 mm radius.
If you change one thing on a drawing today, change the radii: it costs nothing in material or function — a larger radius is stronger, not weaker — and it is the change most likely to cut machine time.
Pocket depth: shallow pockets, shorter tools
Depth is what makes a pocket expensive, because depth decides the tool. A cutting tool is a beam: the longer it sticks out, the more it bends, so a long tool must take lighter cuts and move more slowly. Hubs’ rule is that a pocket should be no deeper than four times its width; Protolabs’ rule for slot-like features is similar — keep the depth below six times the feature width.
The buyer has three ways to fix a pocket that is too deep, in this order. First, ask whether the depth is needed: a 30 mm deep pocket that only needs 15 mm of engagement is 15 mm of cutting time spent for nothing. Second, widen the pocket — a wider pocket takes a larger, stiffer cutter. Third, step the pocket: a wide, shallow upper section and a deeper lower section only where the depth is genuinely needed.
Depth also interacts with the radius rule: a deep pocket with a large radius is still a deep pocket, and a shallow pocket with a tiny radius still needs a tiny cutter. The worked example below shows both rules applied to the same pocket — that is how the saving appears, not from one change but from both.
Walls, tall features, and small details
A wall is a structure, and cutting forces push on it. A thin wall vibrates under the cutter, leaving chatter marks, loosening tolerances, and in the worst case breaking. Hubs recommends a minimum wall of 0.8 mm for metals and 1.5 mm for plastics, with 0.5 mm and 1.0 mm as the feasible limits, noting that plastics need the thicker wall because they warp and soften with heat; Protolabs’ minimum is 0.5 mm. These are minimums, not targets: a wall at the minimum must be cut gently, while a thicker wall or a rib lets the shop cut normally.
Tall features fail the same way: a feature whose height is more than four times its width is prone to vibration, and Hubs recommends keeping the ratio below four. Sometimes the fix is simple — rotate the part by 90 degrees so the tall feature lies down, changing the aspect ratio without changing the part. But it changes the setup, so decide it with the shop.
Small features have their own limit: Hubs recommends keeping features at 2.5 mm or larger, with 0.5 mm as the feasible minimum; anything below that is micro-machining. A 1 mm wide slot needs a tiny cutter and slow feeds, and it is easy to damage in deburring or assembly — so ask whether the function needs it. Engraved text is the classic case: Protolabs notes it is one of the most time-consuming operations, and etching or laser-marking is usually better.
Holes and threads: use standard sizes
A hole with a standard drill diameter can be drilled with a standard drill bit — fast and cheap. A non-standard diameter must be machined with an end mill, and Hubs says to treat it as a cavity, with the pocket depth and radius rules applying. So the first check on any hole is whether its diameter matches a standard drill size; if not, and no mating part drives it, change it.
Depth follows the same logic as pockets. Hubs recommends a hole depth no more than four times the diameter, six times at most; Protolabs gives the same shape of rule — on-axis and axial holes down to 1 mm, maximum depth six times the diameter, and radial holes, drilled from the side, at least 2 mm. A deeper hole needs a longer drill, more pecking to clear chips, and slower feeds. The options are familiar: shorten it, enlarge it, make it a through hole, or drill from both sides.
Threads deserve a short note here. Hubs recommends a thread length no more than three times the nominal diameter, and a size of M6 or larger where possible, with M2 as the feasible minimum. A thread longer than three diameters adds no usable strength, only cutting time and breakage risk. For the method choice — tapped, thread-milled, or insert — and the callout itself, see our guide on how to specify threads on CNC machined parts; its table covers the four methods, and this guide does not repeat it.
Setups: count the faces, not the features
A setup is one clamping of the part on the machine, and it is the unit the shop’s labour is measured in. A part machined in one setup is loaded, aligned and inspected once; a part needing three setups, three times, with manual handling between each. The features do not change — the handling does.
The check is simple: count the faces that carry machined features. Features on one face usually need one setup; on opposite faces, at least two; on five faces, at least three, unless the shop has multi-axis equipment — and multi-axis work costs more. So the design question is not "how many features does this part have" but "how many faces do they sit on": a bracket with ten holes on one face is cheaper than one with three holes on three faces.
Three design moves reduce setups. First, put features on as few faces as possible: move a hole from the side face to the top face if the function allows it. Second, design the part so it can be flipped once rather than re-fixtured three times — a part with a flat back and all features on the front is a one-setup part. Third, if the part genuinely needs features on many faces, split it into two pieces machined in one setup each and assembled. Hubs recommends exactly this: two simple setups cost less than one complex one plus two re-fixturings.
There is a limit: some parts need features on several faces because the assembly demands it. In that case say so in the RFQ, let the shop plan the setups, and ask how many setups the price assumes — a quote that assumes two for a drawing that needs four will be revised, and a revised quote is a delayed order.
Stock size, material, and cosmetic faces
Every machined part starts as a block, bar, or plate, and the shop buys that stock and then cuts most of it away. A part machined from a block twice its size pays for the extra material and the time spent removing it. Choosing stock close to the finished size — the smallest standard size covering the part plus a clamping allowance — is a free saving, so ask the shop what sizes it holds.
Material choice matters too, but it is a function decision first and a cost decision second. Hubs publishes a useful comparison: for the same part, aluminium 6061 is its cheapest metal, alloy steel 4140 costs roughly a quarter more, and among plastics POM (Delrin) is cheapest with ABS roughly half as much again — each dollar-sign step is about a 25% price increase. Those are Hubs’ published relative figures, not a price list: a part that needs steel’s strength cannot be made in aluminium to save money. But where two materials both meet the function, the cheaper one to machine is the cheaper part. Our CNC machining guide covers material selection in more depth.
Cosmetic faces are the last easy saving. A part has faces people see and faces they do not: the first may need bead blasting, anodising, or a fine Ra value, while the rest need only the standard as-machined finish, Ra 3.2 µm. A drawing that asks for a fine finish "all over" pays for precision on faces nobody will ever see — our guide to specifying surface finish on CNC machined parts shows the Ra values and finishes. Mark the cosmetic faces and the finish each needs, and leave the rest at the standard.
Change first: the ranking
Not all changes are equal: some cost nothing and save the most, while others cost a redesign and save little. Ranked by saving against effort:
| Rank | Change | Why it comes first |
|---|---|---|
| 1 | Loosen tolerances that do not affect function | The single largest cost driver on most drawings; costs nothing to change and removes inspection, process control and scrap risk. See our CNC tolerance guide for the ISO 2768 defaults. |
| 2 | Enlarge internal corner radii | Free in material and function, and it decides the cutter size — the largest single effect on machine time. |
| 3 | Reduce the number of setups | Removes manual handling and re-alignment; often achievable by moving features between faces. |
| 4 | Shallow the pockets and thicken the walls | Shorter, stiffer tools and faster cutting; needs a real design decision, so it comes after the free changes. |
| 5 | Standardise hole and thread sizes | Removes special tooling and secondary operations; small effort, steady saving. |
| 6 | Fit the stock size and mark cosmetic faces | A free saving on material and finishing, but smaller than the items above. |
Work down the ranking in order: ranks one and two take minutes and usually move the quote the most. Ranks three to six need design judgement — worth doing, but not before tolerances and radii are fixed.
Worked example: one pocket, before and after
This is an illustration, not a quotation and not a promised saving. It shows how the rules combine on a single feature. The numbers are chosen to make the mechanism visible; real cutting time depends on the shop’s tooling, material, machine, and feeds and speeds, which this example does not state. Confirm any change with the shop that will make the part.
Take an aluminium bracket with one rectangular pocket, 40 mm long and 30 mm wide, that holds a mating block. The first drawing calls for a pocket 30 mm deep with 1 mm internal corner radii; the second, the same pocket 20 mm deep with 10 mm radii — the mating block only engages the top 20 mm, and its own corners are rounded to 10 mm.
| Before | After | |
|---|---|---|
| Pocket size | 40 × 30 mm | 40 × 30 mm |
| Pocket depth | 30 mm | 20 mm |
| Internal corner radius | 1 mm | 10 mm |
| Cutter the radius allows | 2 mm diameter at most | 20 mm diameter |
| Cutter length needed | At least 30 mm of reach | 20 mm of reach |
| Against Hubs’ rules | 1 mm radius is far below one third of the 30 mm depth | 10 mm radius is half the 20 mm depth, well above the one-third rule |
| What the shop must do | Cut with a long, thin 2 mm cutter, in many shallow passes, at slow feeds, with vibration and breakage risk; Protolabs notes a 1 mm cutter is limited to pockets about 9.52 mm deep, so a 30 mm deep pocket with 1 mm corners cannot be cut with that tool at all in one reach | Rough the pocket with a short, rigid 20 mm cutter in a few deeper passes, then finish the corners with the same cutter on a circular path |
The mechanism is the whole point. The before design forces the smallest, longest, most flexible tool the shop owns, and that tool sets the speed for the entire pocket. The after design uses a cutter ten times the diameter and a third shorter, removing far more material with each pass. Nothing about the part’s function changed — only two numbers on the drawing did.
Two cautions belong with the example. First, the saving is in machine time, not in a percentage — no percentage is claimed, because the actual time depends on feeds, speeds, and the rest of the part. Second, the redesign was only possible because the depth and radius were not driven by the function: if the mating block genuinely needs 30 mm of engagement, the pocket must stay as drawn.
Pre-quote drawing checklist
Run through this list before the drawing leaves your desk — a shop that receives all of it can quote without a round of clarification questions.
| # | Item | What to state |
|---|---|---|
| 1 | STEP file and 2D drawing | Current revision, with the material grade named |
| 2 | General tolerance | ISO 2768 class in the title block, so unmarked dimensions have a defined tolerance |
| 3 | Critical tolerances only | Tight limits flagged on the dimensions that affect fit, function, sealing or alignment; the rest on the default |
| 4 | Datum scheme | Datums stated, so the supplier and the inspector measure from the same origin |
| 5 | Corner radii | One radius for all internal corners, larger than one third of the pocket depth |
| 6 | Pocket depths and wall thicknesses | Against the rules in the table above, with any exception noted and its reason given |
| 7 | Hole and thread sizes | Standard drill and thread sizes; thread size, pitch, class, thread depth and drill depth stated separately |
| 8 | Setups | Features on as few faces as possible; note any face that must be machined separately |
| 9 | Cosmetic faces | Marked, with the finish each one needs; the rest left as-machined |
| 10 | Quantity, finish and inspection | Batch size and expected repeat orders, finish per surface, and what inspection evidence is required |
| 11 | DFM note requested | Ask the shop to flag, with the quote, any feature it would change and why |
That last item is the cheapest insurance in the list: a shop asked for a DFM note will tell you about the radius it would enlarge and the setup it would remove — before the order, when the change is free. If the part is new, tight-tolerance, or safety-critical, prove the drawing on a sample first: our guide on whether to order a CNC sample before volume production explains what a sample must prove and what evidence to require.
Frequently asked questions
Can I just ask the shop to fix the design for me?
You can ask, and a good shop will suggest changes — but only you know which features your function needs. Send the drawing with the rules applied, and ask the shop to confirm or correct them.
Will enlarging a corner radius weaken the part?
No — the opposite. A sharp internal corner concentrates stress, and a larger radius spreads it, so a larger radius is stronger as well as cheaper to machine. The only reason to keep a small radius is a mating part with a square corner — the fix is an undercut.
My part really does need a deep pocket and a small radius. What then?
Keep the design and pay for it — but say so in the RFQ, and ask whether a stepped pocket or a split part would do the same job at lower cost.
Send the drawing for a DFM review before you ask for a quote
The cheapest moment to change a machined part is before the quote, when the change is a number on a drawing. Send the STEP file and the 2D drawing with the radii, pocket depths, tolerances, cosmetic faces and setups already decided, and ask for a DFM review with the quote. Contact Cavity Mold with the part files, the material, the quantities, the critical tolerances, the cosmetic faces, the finish, the delivery region and timing.