
Key takeaway: The seven basic injection molding components are material, mold, injection unit, clamping unit, temperature control, ejection, and inspection/process control.
A practical seven-part framework
There is no single official universal taxonomy for the ‘seven components’; this is a practical framework for reviewing a molding system. It keeps the discussion connected from resin to finished, inspected part.
The seven components
Each component has a distinct role, but quality depends on how the interfaces work together.
- Material: the specified resin, grade, drying, lot, additives, and regrind policy.
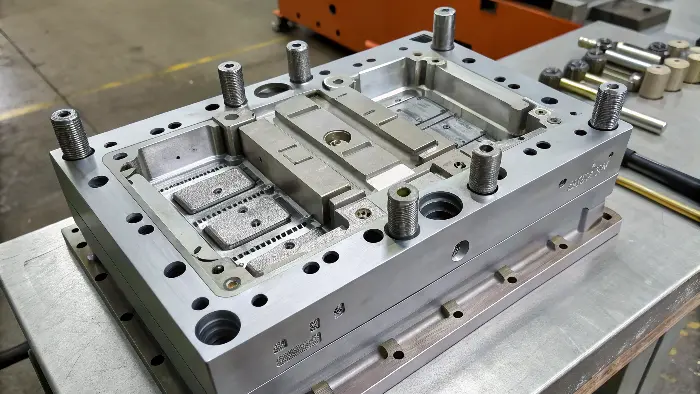
- Mold: cavity, core, gates, runners, vents, cooling, parting line, and maintenance.
- Injection unit: hopper, barrel, screw, nozzle, dosing, mixing, and pressure control.
- Clamping unit: platen, mold support, alignment, clamp force, and mold protection.
- Temperature control: heaters, cooling circuits, flow, sensors, and stable thermal conditions.
- Ejection: pins, sleeves, stripper, air, release, and safe part handling.
- Inspection and process control: settings, measurement, traceability, alarms, and change control.
Why the framework matters
A defect often crosses component boundaries: a short shot may involve material, injection, venting, clamp alignment, or temperature; warpage may involve mold design, cooling, material, and process. Reviewing the seven components makes troubleshooting more systematic and helps buyers ask for complete evidence.
Frequently Asked Questions
Are these seven components an official industry standard?
No. They are a practical checklist. Different engineers may group machine, mold, material, utilities, and quality functions differently.
Which component affects part quality the most?
All seven interact. Geometry, resin, mold, machine, temperature, ejection, and inspection must be coordinated for repeatable results.
How can a buyer use this framework?
Use it to structure DFM, equipment review, process approval, troubleshooting, maintenance, and supplier questions so no major control area is missed.
Related Cavity Mold Services
Engineering and DFM; Mold making; Plastic injection molding; Contact Cavity Mold.
Have a drawing, resin, finish, volume, or quality requirement to review? Contact Cavity Mold for a project discussion.
Reference material
See the molding system as connected interfaces
An injection molding system is more than a press. Part quality emerges from the interfaces among material handling, plasticizing, injection, clamping, mold, cooling, and control or inspection.
| Decision | Evidence to review | Boundary |
|---|---|---|
| 1–2 Material and plasticizing | Store, dry, blend, melt, and meter the selected material. | Material condition and thermal history enter the process here. |
| 3–4 Injection and clamping | Fill, pack, and hold the mold closed with repeatable force and motion. | Machine capability must fit the part and mold. |
| 5 Mold | Create the part geometry, flow path, vents, cooling, and release. | Tool architecture influences every later setting. |
| 6–7 Cooling and control | Remove heat, monitor inputs, inspect outputs, and react to drift. | A process without feedback is difficult to sustain. |
System-learning path
- Trace one part from material receipt to release.
- Identify which component controls each CTQ.
- Ask suppliers for the evidence at each interface.
- Record the gaps before choosing a machine or tool.
Use engineering for the part-specific interfaces and mold-making for the tool contribution.