
PMMA automotive lighting parts require optical-grade material control, dry resin, polished tooling, balanced filling, cooling, low stress, and validated appearance. Lenses, covers, and light guides must meet optical, dimensional, environmental, and assembly requirements at the same time.
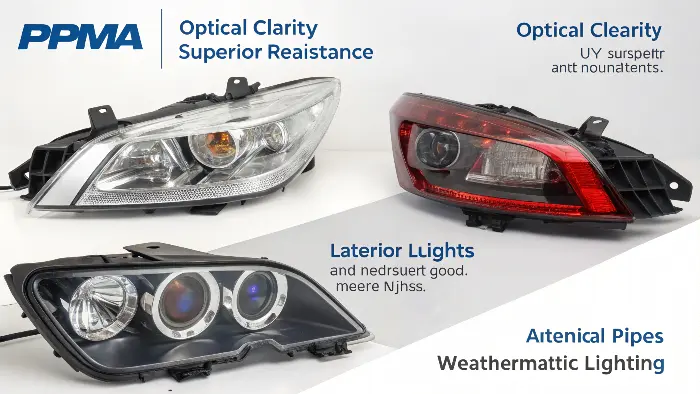

Automotive lighting risks
- Haze, bubbles, splay, contamination, weld lines, flow marks, and birefringence can affect light transmission or appearance.
- Warp, sink, shrinkage, or cavity imbalance can change optical geometry and assembly fit.
- Heat, UV, weathering, chemical exposure, vibration, and impact requirements may rule out a general-purpose grade.
- Gate vestige, ejector marks, parting lines, and texture must be controlled in visible zones.
Tool and process controls
Use the exact optical-grade or heat-resistant PMMA data, controlled drying, clean material handling, polished steel, balanced gates, adequate venting, thermal balance, and a low-stress process window. Validate transmission, haze, color, beam or light distribution, dimensions, stress, and environmental performance according to the customer’s specification.
Supplier questions
Ask how the supplier measures optical performance, controls contamination, records resin lots, protects polished surfaces, and requalifies after a material, mold, or process change. A clear sample under one light is not a complete automotive approval.
Plan the next step
Share your part, resin, annual volume, critical dimensions, finish, and timing with the Cavity Mold team through our contact page. We can review the manufacturing risks and recommend a practical next step.
Related Cavity Mold resources
- Plastic injection molding services
- Injection mold engineering services
- Injection mold making services
- Contact Cavity Mold
Technical references
- Röhm PLEXIGLAS automotive lighting materials
- Mentor Automotive optical injection molding
- ENGEL optical injection molding equipment
Translate the lighting function into molding controls
A lighting component can be a lens, light guide, cover, reflector interface, or cosmetic housing. Each role changes the importance of transmission, haze, birefringence, geometry, surface, heat, UV, weathering, impact, and assembly fit.
| Decision point | Check | Evidence or boundary |
|---|---|---|
| Optical function | Define path, angle, surface, thickness, and light distribution. | Plan optical measurement or agreed appearance method. |
| Environment | Define heat, UV, weathering, chemicals, vibration, and impact. | Use grade data and customer-defined validation. |
| Tool and process | Review gates, welds, ejection, parting, polish, cooling, and stress. | Plan DFM, trial evidence, and cavity identity. |
| Assembly | Define dimensions, clips, seals, coatings, and interfaces. | Plan functional fit and dimensional inspection. |
Application requirement map
- Separate optical, dimensional, and environmental requirements.
- Name the evidence owner for each requirement.
- Put material and validation assumptions in the RFQ.
- Do not infer approval from a clear appearance sample.
Define these requirements in the RFQ and use engineering review to keep lighting function visible.