Reducing injection mold costs without compromising quality means removing avoidable complexity while protecting function, tool life, process capability, and inspection evidence. The best savings usually come from decisions made before steel is cut, not from deleting controls after production starts.
Seven cost-control levers
- Resolve draft, walls, ribs, gates, cooling, ejection, and tolerance conflicts in early DFM.
- Simplify slides, lifters, deep pockets, shutoffs, and surface requirements where the part function allows it.
- Choose cavity count from real volume, machine fit, balance, inspection, maintenance, and ramp-up demand.
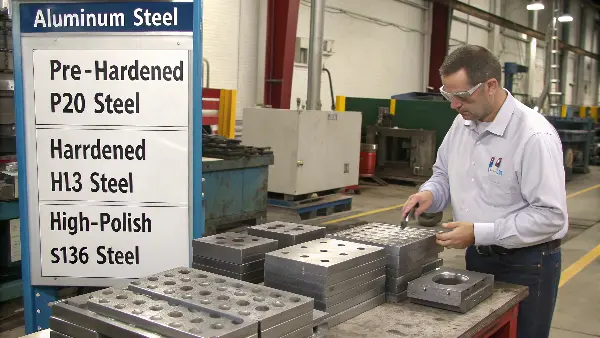
- Select steel and inserts by resin wear, corrosion, polish, texture, volume, and repair risk.
- Standardize mold bases, components, datums, inserts, and spare parts without forcing an unsuitable design.
- Define surface finish and texture by customer need rather than paying for an unclear premium.
- Validate early with an agreed trial, dimensional report, appearance standard, and process window.
Protect quality while reducing spend
Maintain CTQs, measurement capability, cavity identification, material traceability, maintenance access, and change approval. A cheaper mold that requires frequent hand fitting, produces unstable parts, or cannot be repaired economically may have a higher lifecycle cost.
Compare total cost
Include tooling, material, machine time, scrap, correction loops, logistics, downtime, maintenance, and future changes. A transparent assumption list makes a lower-cost proposal easier to trust.
Plan the next step
Share your part, resin, annual volume, critical dimensions, finish, and timing with the Cavity Mold team through our contact page. We can review the manufacturing risks and recommend a practical next step.
Related Cavity Mold resources
- Injection mold making services
- Injection mold engineering services
- Plastic injection molding services
- Contact Cavity Mold
Technical references
- Protolabs Network injection molding cost and design guide
- Protolabs design-for-moldability toolkit
- Xometry injection mold lifespan reference
Validate savings before you approve the change
A lower tooling cost is useful only when the requirement, risk owner, and acceptance evidence stay visible. Treat each proposed saving as an engineering change request rather than an automatic improvement.
| Decision point | Check | Evidence or boundary |
|---|---|---|
| Fewer cavities or a smaller mold base | Check annual volume, machine fit, balance, sampling, and expansion path. | Do not trade capacity or maintenance flexibility for an untested headline saving. |
| Simpler action or parting strategy | Review release direction, draft, shutoff function, flash risk, and operator access. | A cheaper concept can create manual rework or a late repair. |
| Different steel or insert construction | Check resin wear, corrosion, polish, expected service, and repair route. | State the duty and maintenance assumption instead of claiming a universal life. |
| Reduced inspection or trial scope | Define CTQs, measurement method, sample identity, and approval owner. | A saving is incomplete if variation is merely discovered later. |
A practical value-engineering record
- State the original requirement and proposed change in one sentence.
- Assign owners for function, tooling, process, quality, and commercial approval.
- Record what will be measured, on which sample, using which method.
- Approve the saving only after the acceptance boundary still holds.
Use an engineering review to separate a genuine simplification from a change that only moves cost downstream. When you request a quote, send the approved boundary through a comparable RFQ.