PTFE part design must begin with the correct forming route because pure PTFE is not processed like a conventional melt-flow injection molding resin. Most pure PTFE parts use powder preforming and sintering, followed by machining where needed; melt-processable fluoropolymers such as PFA or FEP may be alternatives when injection-molded geometry is required.


Choose the manufacturing route
- Compression and sintering: suitable for many PTFE shapes, with tooling and furnace cycles designed around preform density, shrinkage, and sintering.
- Ram or paste extrusion: useful for continuous profiles, tubes, or stock shapes that can be machined later.
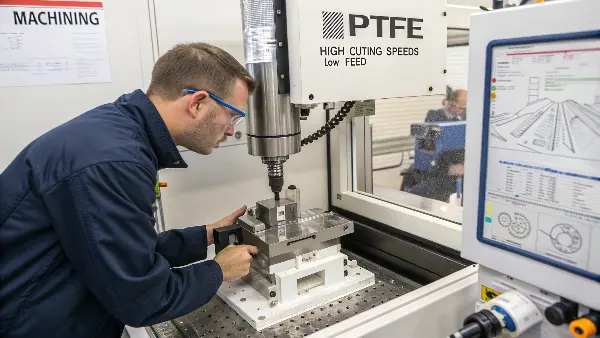
- CNC machining: appropriate for prototypes, complex details, and parts made from molded stock, while accounting for PTFE movement and tolerance.
- PFA or FEP injection molding: possible when the application can use a melt-processable fluoropolymer rather than pure PTFE.
Engineering checks
Define temperature, chemicals, friction, wear, pressure, electrical requirements, dimensional stability, and service life. Account for PTFE’s high thermal expansion, creep, shrinkage, filler selection, porosity risk, and post-sinter machining. Avoid thin unsupported features, sharp transitions, and tolerances that the selected process cannot hold consistently.
What to request from a supplier
Ask for the exact resin or compound, forming method, shrinkage data, sintering cycle, inspection method, machining allowance, surface finish, and application-specific compliance evidence. Do not approve a “PTFE injection mold” from the material name alone; confirm whether the proposal is compression-sintering, a modified fluoropolymer, or another process.
Plan the next step
Share your part, resin, annual volume, critical dimensions, finish, and timing with the Cavity Mold team through our contact page. We can review the manufacturing risks and recommend a practical next step.
Related Cavity Mold resources
- Injection mold engineering services
- Injection mold making services
- Plastic injection molding services
- Contact Cavity Mold