ABS injection molding is commonly used for housings, covers, trim, and functional components because the material can combine impact performance, stiffness, appearance, and practical moldability. The exact ABS grade still controls drying, melt temperature, mold temperature, shrinkage, chemical resistance, color, and any flame or application requirement. Do not treat “ABS” as a complete material specification.

What should be defined before molding ABS?
- Exact grade, color, additives, recycled-content limit, and required surface finish.
- Impact, stiffness, temperature, chemical, UV, electrical, or plating requirements based on the product function.
- Nominal wall, flow length, ribs, bosses, snap features, inserts, texture, gate location, and critical dimensions.
- Annual volume, batch size, machine, cavity count, inspection method, and packaging.
SABIC’s CYCOLAC ABS product information shows why grades must be selected for the required balance of impact, flow, appearance, and application performance. Use the selected grade’s data sheet for the final process window.

ABS part and mold design
Walls, ribs, bosses, and draft
Keep walls as uniform as the design allows and core out thick bosses. Use ribs to add stiffness without creating heavy sections that sink or cool slowly. Add radii at corners and draft on draw surfaces. Snap fits and living features should be reviewed for strain, knit lines, ejection, and the orientation of the molded part.
Gates, vents, and surface appearance
ABS can reproduce a good surface, but narrow gates, poor venting, unstable injection speed, and local cold spots can create flow marks, weld-line weakness, burn marks, or gloss variation. Put gates where the fill path supports the functional and cosmetic requirements. Mark areas where a gate vestige or weld line is unacceptable before tooling.
Material preparation and process control
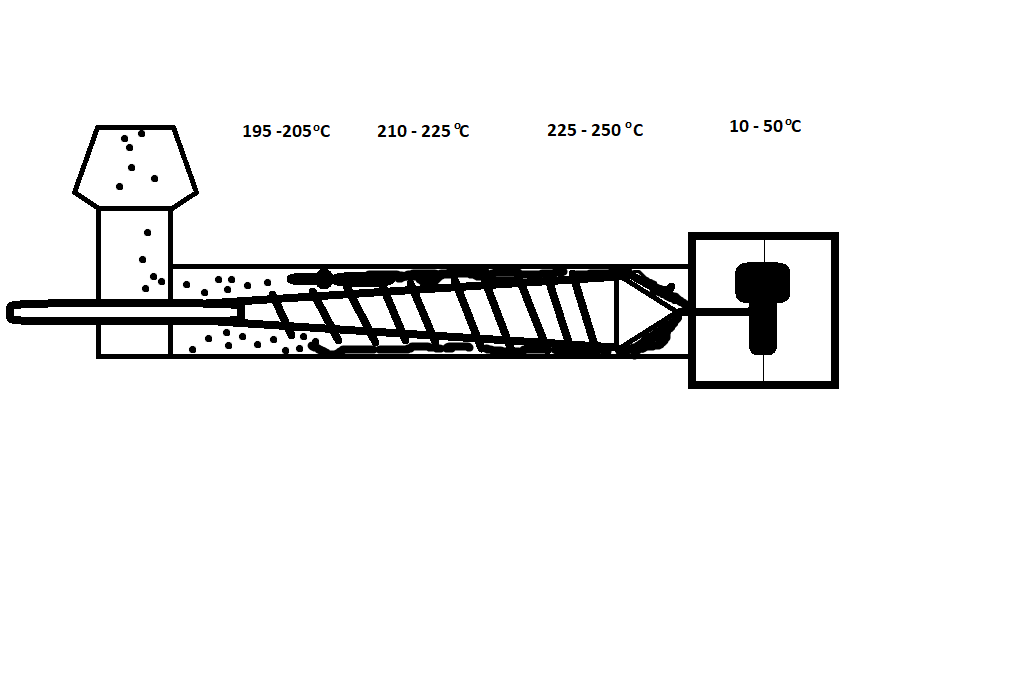
ABS can absorb moisture under unfavorable storage conditions, and moisture may become visible as splay or surface defects. Keep opened material protected and follow the selected grade’s drying guidance. Control barrel residence, screw speed, melt temperature, mold temperature, injection profile, packing, cooling, and recovery. A process sheet should record the actual settings and the measured part results.
Higher mold temperature can improve surface reproduction and weld-line strength in some grades, but it can also change cycle time and shrinkage. Select settings from the grade data and a trial rather than using a generic online number.
Common ABS molding problems
| Problem | Likely contributors | Investigation |
|---|---|---|
| Splay or silver streaks | Moisture, contamination, excessive shear, or thermal degradation | Drying, storage, purge, screw speed, barrel temperature, and residence time |
| Sink or voids | Heavy sections, insufficient packing, early gate freeze, or poor cooling | Wall and boss design, gate size, part weight, cooling, and hold time |
| Weld-line weakness | Flow fronts meeting in a stressed region, cold material, or poor venting | Gate and vent locations, mold temperature, weld-line position, and functional test |
| Warp or dimension drift | Uneven wall, cooling imbalance, material lot, or process change | Cooling circuit, part orientation, cavity data, and conditioning state |
Use Cavity Mold’s engineering support, injection molding service, and mold-making service for a coordinated review. Contact the team with the ABS grade, CAD, annual volume, appearance requirements, and critical dimensions.
Write the ABS grade brief before quoting
Expand ABS into the requirement that drives the grade: impact, stiffness, gloss, texture, plating, flame performance, UV exposure, chemical resistance, color stability, or recycled-content limit. A grade that fills easily may not satisfy a stress or appearance requirement, and additive changes can alter shrinkage and surface behavior.
| Product need | Process and mold questions |
|---|---|
| Cosmetic housing | Where are weld lines, gate marks, texture transitions, and read-through risks acceptable? |
| Snap-fit or structure | What load, assembly cycle, radius, and chemical exposure must be demonstrated? |
| Plated or coated part | Which surface preparation, allowance, and inspection method apply? |
Use the exact supplier data sheet for drying, melt temperature, mold temperature, and shrinkage. Record moisture practice, lot, fill profile, cooling, color, and defect locations during sampling. Use the materials page for the shortlist and the engineering review for wall, gate, vent, and cosmetic maps.