
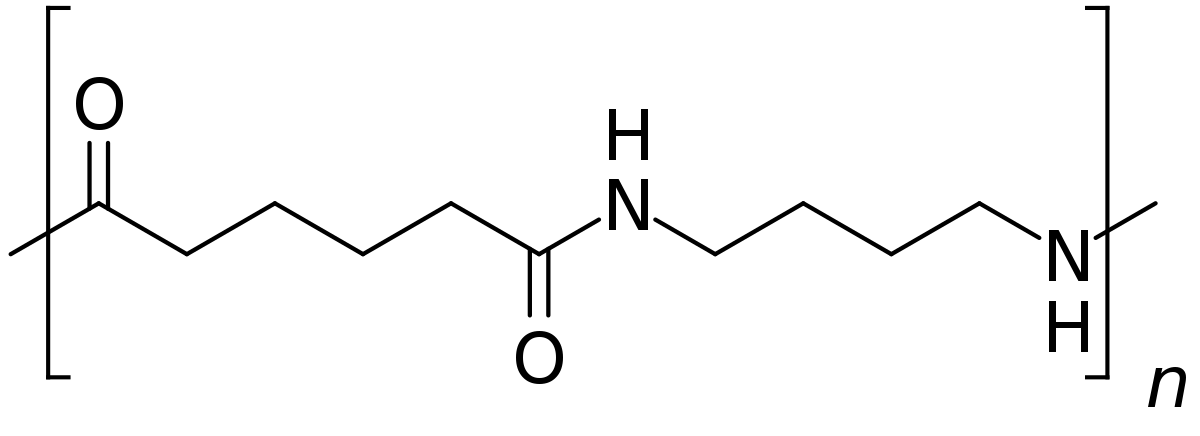
PA66 injection molding requires disciplined moisture control, grade-specific processing, and a design that accounts for shrinkage, conditioning, and—when reinforced—fiber orientation. PA66 is not interchangeable with PA6 or with every nylon grade. The exact polymer, reinforcement, heat stabilizer, color, and end-use environment must be specified before tooling.
PA66 material preparation
Polyamide absorbs moisture from the environment. Excess moisture can cause splay, bubbles, reduced molecular weight, surface defects, or inconsistent mechanical performance. Keep bags sealed, use a suitable dryer when required, and record hopper condition, drying time, temperature, dew point, and material exposure.
BASF’s Ultramid PA66-GF35 processing data sheet demonstrates that drying, melt temperature, mold temperature, residence time, and shrinkage are grade-specific. Use the selected supplier’s data sheet rather than copying a generic nylon setting.
PA66 part and mold design
Wall thickness and shrinkage
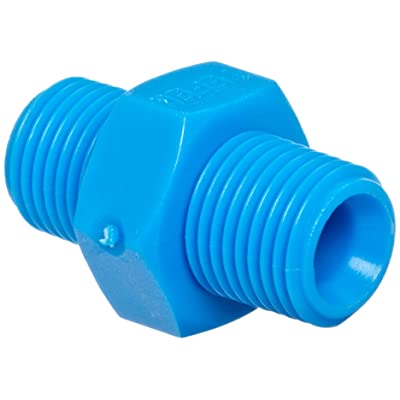
Keep walls consistent, core out heavy intersections, and use radii at corners. Unfilled and glass-filled PA66 can have different shrinkage and orientation behavior. Moisture conditioning after molding can also change dimensions, so critical tolerances must state the conditioning state and measurement method.
Ribs, bosses, and inserts
Ribs and bosses should support function without creating thick regions that sink or cool slowly. For inserts, consider thermal expansion, stress concentration, pull-out, and the direction of fiber or flow. Gate and weld-line locations should be reviewed against the load path.
Process and mold controls
- Control melt and mold temperature within the selected grade’s window; mold temperature affects crystallization, shrinkage, surface, and cycle.
- Use gates and runners that fill the part without excessive shear or premature freeze.
- Vent the end of fill and deep features; trapped air can cause burns, short shots, and weak weld lines.
- Balance cooling around thick sections and monitor cavity-to-cavity dimensions.
- Review steel wear and screw or check-ring suitability for glass-filled grades.
- Record recovery, cushion, fill, pack, cooling, part weight, dimensions, and startup behavior.
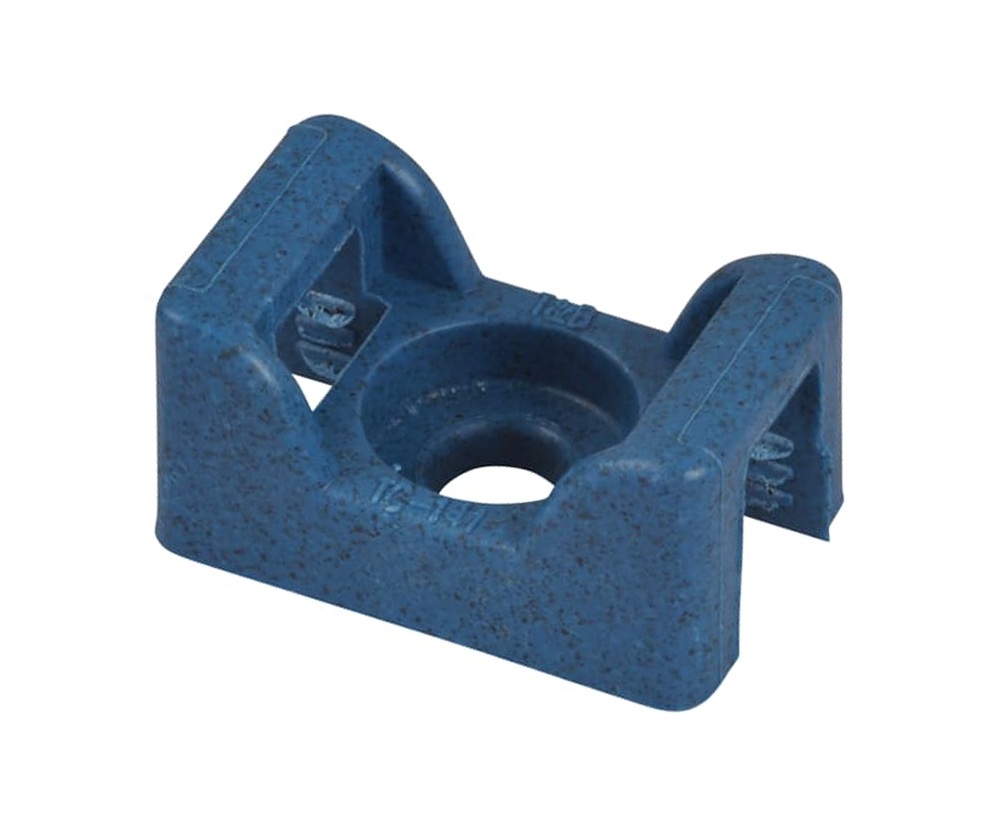
PA66 quality checklist
| Requirement | Validation |
|---|---|
| Material | Exact grade, reinforcement, color, moisture record, lot traceability, and approved alternatives |
| Dimensions | Critical dimensions, flatness, hole position, shrinkage direction, and conditioning state |
| Appearance | Splay, weld lines, fiber read-through, flash, sink, burns, and gate vestige |
| Function | Load, fit, torque, wear, heat, chemical, humidity, and life tests as required |
For a coordinated PA66 program, see Cavity Mold’s engineering service, injection molding service, and mold-making service. Contact the team with the exact grade, CAD, volume, and inspection plan.